Eight common flexo print defects what causes them, and how to correct them on press.
This guide sets out the eight print defects our technical team is called out to most often. Each entry describes what the defect looks like on the printed web, lists the probable causes in the order worth checking them, and gives the corrective action.
If you still have questions our technical service team supports customers across Europe, the Middle East and Africa directly on site.
Before you change anything: work the variables in order
Changing three settings at once tells you nothing about which one fixed the problem. When a defect appears mid-run, isolate it in this sequence:
- The ink. Check viscosity against the job standard first. Then check solvent balance and the condition of the ink, contamination and how long the ink has been circulating.
- The transfer. Anilox cell volume and condition, doctor blade type, angle and pressure, printing plate inspection for manufacturing defects or surface wear, verification of plate hardness and relief depth. Mounting tape, type and hardness.
- The machine. Impression settings between plate cylinder, anilox and substrate; web tension; dryer performance; chill drum function.
- The substrate. Corona treatment level and age of the film, surface cleanliness, thickness tolerance, wetting behaviour.
Potential Issues
What you see:
The ink does not adhere sufficiently to the substrate and can be removed easily, typically failing a tape test.
Adhesion failures are the most commercially serious defect on this list, because they often pass visual inspection at the press and are only discovered downstream at lamination, filling or in the customer's hands. Treat surface energy and ink system compatibility as your first two checks.
Start here:
Measure the film's surface tension before adjusting anything on the press. Corona treatment decays with time in storage, and an under-treated or aged film will defeat every other correction you make.
Potential issues & solutions
What you see:
The ink adheres to the reverse side of the film and causes damage when the substrate is unwound.
Blocking is a heat-and-solvent problem. It is nearly always the result of ink that has not fully released its solvent before the web is wound, or of a reel that is wound too tightly, too warm, or both.
Start here:
Measure the web temperature at the winder. If the film is going into the reel warm, no adjustment to the ink will solve the problem.
Potential issues & solutions
What you see:
Very faint images of the design appearing in solid areas of the print. The defect shows up when a solid background carries negative elements — reversed text, windows, cut-outs.
Ghosting is an ink starvation phenomenon. The anilox cannot deliver enough ink to the solid area immediately following the negative element, and the shortfall reproduces as a faint echo of the shape that caused it.
Start here:
Inspect the anilox for cell blockage before changing the ink. A partially plugged roll starves the plate in exactly the pattern that produces ghosting.
Potential issues & solutions
What you see:
Small areas where ink has pulled back from the substrate, leaving unprinted or light points within a solid.
Pinholes are a wetting failure. The ink is being applied but will not hold as a continuous film either because the surface rejects it, or because the ink film is too thin to level.
Start here:
Use the correct hardness tape and increase the printing pressure and the ink film thickness. if you are running water-based inks, check pH first. It drifts steadily through a long run and takes wetting behavior with it.
Potential issues & solutions
What you see:
A thin outline or halo around printed images, screen dots or text, usually denser than the main image.
The halo is squeezed ink. Excess pressure or excess volume forces ink out beyond the edge of the printing element, where it deposits as a ring. It is almost always a pressure and volume problem, not an ink problem.
Potential issues & solutions
What you see:
A mottled or marbled appearance across solid print areas — the ink layer is visibly uneven rather than flat.
Mottling points to inconsistent ink transfer or an uneven contact surface. Work through the plate, then the ink body, then the substrate.
Potential issues & solutions
What you see:
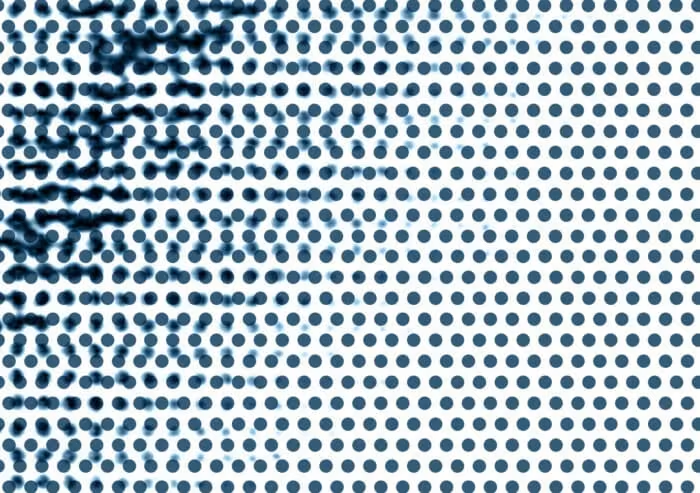
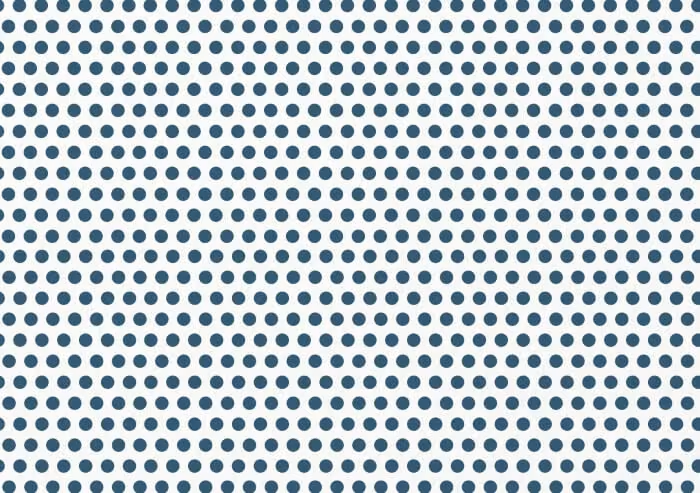
Ink connections forming between individual screen dots on the printing plate. The depressions between dots fill with ink and the halftone closes up.
Bridging is a drying-speed and viscosity problem. The ink is becoming too tacky on the plate before it transfers, or there is simply too much of it for the screen ruling being run.
Potential issues & solutions
What you see:
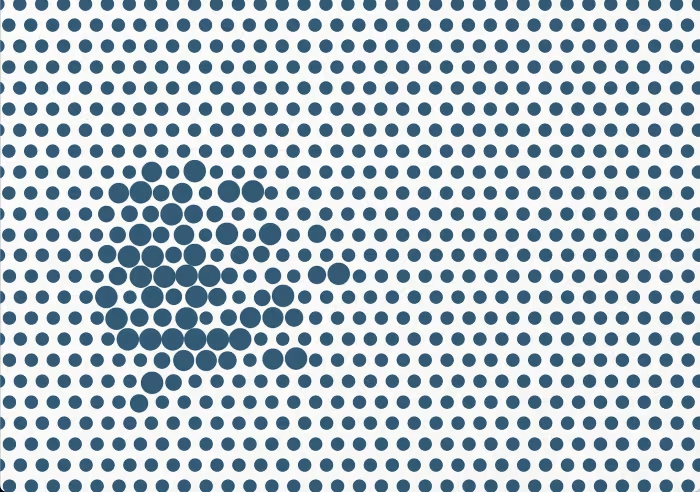
Excessive dot gain on the substrate, reducing detail and flattening contrast across the image.
Some dot gain is inherent to flexography and is compensated for in prepress. The defect is gain beyond what the curve accounts for which is a mechanical problem, not a design one.
Potential issues & solutions
Our technical support is here to help
DF Inks’ technical service team works on site with converters across Europe, the Middle East and Africa, supported by our own laboratories and production facilities in Greece, Romania and Nigeria. We formulate the ink, so we can customize it for converters not just recommend a workaround.
FAQs about flexographic printing defects
The most common causes are insufficient corona treatment on the film, an ink system that does not match the substrate, inadequate drying, and surface contamination. Check the film's treatment level first, corona treatment decays during storage, and an aged film will fail a tape test regardless of ink performance.
Ink mottling comes from uneven ink transfer. Check the plate surface for damage or clouding, then ink viscosity in both directions, too low and too high both produce it, then contamination on film, and finally doctor blade pressure.
Many can be corrected in-run, particularly viscosity, doctor blade pressure and dryer settings. Defects rooted in the plate, anilox condition or substrate batch require a stop. Change one variable at a time and record the result, simultaneous adjustments make the cause impossible to identify.